
Thermodynamic boiler optimisation through HTC solid-body radiation
- Sector focus
- Infrastructure, Energy & Logistics
- Document classification
- Anonymised technical report
- Technology
- HTC retrofit (solid-body thermal radiation)
- Plant specification
- Shell boiler (natural gas H)
- Procedure
- TÜV-validated efficiency measurement during ongoing operation
- Plant type
- High-temperature hot water boiler, 499-2,440 kW
- Fuel
- Natural gas H
- Measurement method
- Before-and-after comparison (TÜV-validated)
- Evidence
- Increase in primary energy efficiency & emission reduction
- Status
- Verified & released - AZ: JB02WP16
DOCUMENTATION & TECHNICAL REPORT
MANAGEMENT SUMMARY
This technical report documents the technical and commercial optimisation of a boiler plant in the infrastructure, energy & logistics sector through the use of high-temperature ceramics (HTC). The results are representative of boiler processes in logistics centres, energy plants and large-scale infrastructure facilities.
The validated performance indicators
- Total return advantage
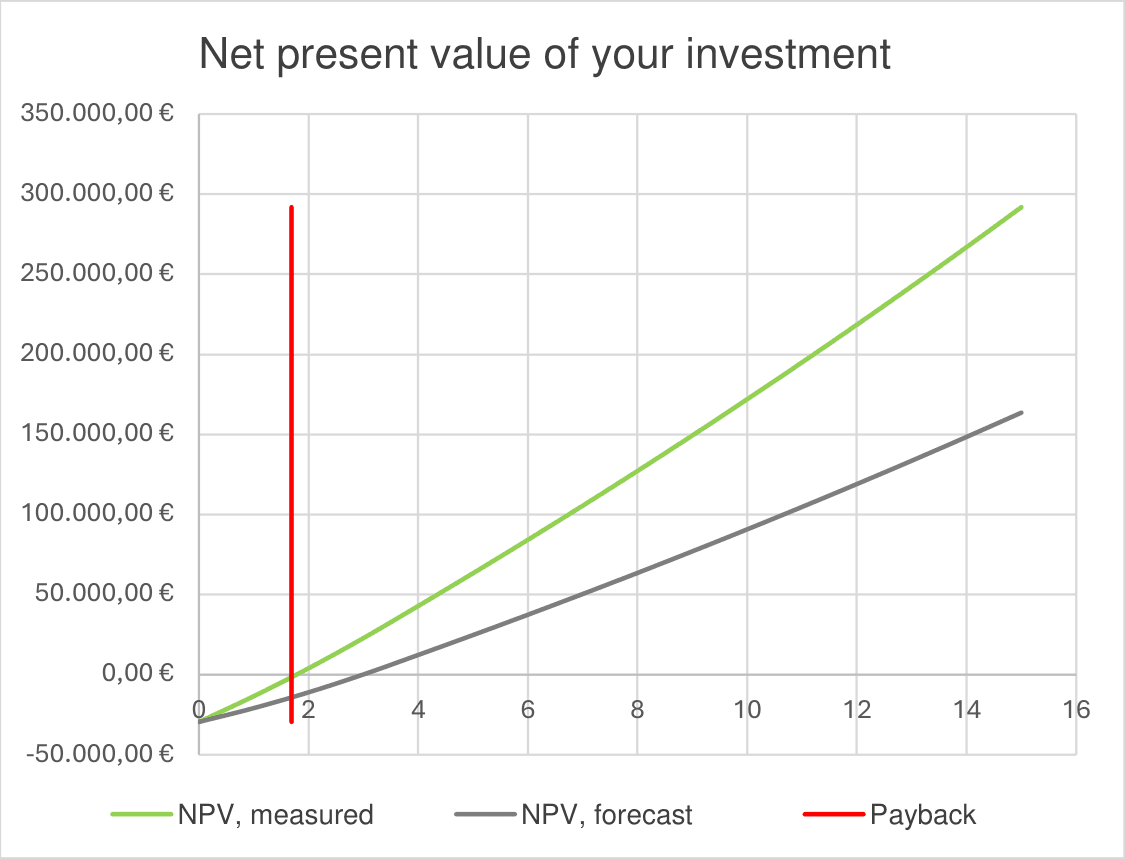
- > €291,000over the remaining service life of the plant.
- Primary energy saving
- > €13,600 p.a.at constant output.
- Payback (ROI)
- 1.69 years(achievable at short notice, without a budget-intensive major investment).
- Cost of Delay
- Avoidance of a liquidity loss of approx. €1,134 per month through immediate implementation.
- Freedom from damage
- 100 % damage-free integration downtimes.
1. Initial situation & challenge
Logistics centres, energy suppliers and infrastructure operators are subject to enormous cost pressure while facing uncompromising requirements for security of supply. The boiler plants for heat and steam generation form the energy backbone here.
In practice, however, conventional boiler systems reach a physical limit – the thermodynamic gap. Incomplete heat transfer in the combustion chamber leads to excessive flue gas temperatures, unnecessarily high cycling rates and inefficient fuel consumption.
The conventional solution – a structural retrofit or complete replacement of the plant – is often ruled out by the technical management. The reasons: high CapEx requirement (capital expenditure) and the unacceptable risk of incalculable plant shutdowns.
Never touch a running system!
2. The solution - minimally invasive integration (HTC)
To remedy this inefficiency without structural intervention, the thermodynamic retrofit procedure of Intensatec was applied in the present case. Custom-made high-temperature ceramics (HTC) are integrated minimally invasively into the combustion chamber of the existing boiler plant.
This physical modification fundamentally changes the radiation dynamics inside the boiler chamber.
- Heat transfer: The ceramic elements absorb the energy of the flame and radiate it in concentrated form onto the water-bearing boiler walls.
- Cycling rate reduction: The boiler holds its temperature significantly longer, which drastically reduces the energy-intensive, constant switching of the burner on and off.
- Emission reduction: Optimised combustion and reduced cycling rates lower the output of CO₂ and NOₓ measurably.
3. The proof - hard facts from plant operation
Current measurement data from plant operation prove that this thermodynamic effect works in practice and translates into hard cash flow.
In all measurements carried out to date on boiler plants up to 110 °C flow temperature, results between +10 % and +17 % were achieved.
The forecast of 8.00 % for the plant presented here was clearly exceeded, with an actual gas reduction of 17.58 %.
4. Installation and verification with full security of supply
For critical infrastructure, an interruption of process heat is absolutely unacceptable. Installation into the existing boiler is carried out minimally invasively.
In high-temperature hot water boilers (above 110 °C flow temperature), the decisive proof of efficiency is provided by a TÜV-validated measurement procedure directly during ongoing operation and takes only two to three hours before and after installation. (Note for steam boilers: here the optimisation potential is determined by means of a well-founded, individual thermodynamic plant analysis).
The measure is contractually secured.
Should the savings calculated in advance not be achieved during the measurement, the client has the right to a fair renegotiation or to damage-free removal with refund of the purchase price. To date, however, this option has never had to be exercised.
5. Conclusion
Before operators consider CapEx-intensive new acquisitions, a thermodynamic look at the existing plant is worthwhile. Anyone who unlocks their unused boiler potential makes a substantial contribution to ESG targets and immediately protects their budget against the price spiral of CO₂ and energy costs.
Validated measurement report (anonymised)
The following extract from our original measurement report documents the effectiveness of the HTC integration in black and white. For your commercial assessment, these three factors are particularly decisive:
1. Optimisation of the cycling rates (burner running time)
Constant switching on and off consumes the most energy. The measurement report shows markedly improved thermal behaviour: with identical burner running time (60 minutes in both measurement cycles), a higher useful heat quantity was generated with simultaneously massively reduced gas consumption.
2. Reduction of the flue gas temperature
The temperature at the chimney fell from 133.90 °C to 108.30 °C. The heat is now transferred to the boiler water in concentrated form by the ceramic instead of escaping unused.
3. Hard ROI through primary energy saving
System efficiency rose from 7.741 kWh/m³ to 9.391 kWh/m³. This corresponds to an increase in energy yield of 21.32 %. The actual reduction in gas consumption, adjusted for weather and consumption, is 17.58 %.
Extract from the measurement protocol
(Plant: high-temperature hot water boiler, natural gas H, 499 – 2,440 kW)
Meter readings and efficiency (comparison over a 90-minute measurement cycle):
| Measurement run | Gas consumption | Heat quantity | Efficiency |
|---|---|---|---|
| Measurement run 1 (without installations) | 83.40 m³ | 645.56 kWh | 7.741 kWh/m³ |
| Measurement run 2 (with HTC installations) | 73.10 m³ | 686.49 kWh | 9.391 kWh/m³ |
- Confirmed increase in energy efficiency
- 21.32 %
- Actual reduction in gas consumption
- 17.58 %
Emission reduction (in relation to the real mass):
| Emission | Reduced by |
|---|---|
| CO₂ (carbon dioxide) (linear to gas consumption) | 17.58 % |
| CO (carbon monoxide) | 30.26 % |
| NOₓ (nitrogen oxides) | 3.50 % |
Economic efficiency calculation:
- Fuel costs p.a. (net)
- €77,431.05
- Consumption reduction p.a. in the 1st year
- €13,612.38
- Payback of the system
- after 1.69 years
- Calculated cost saving (15 years)
- €235,404.53
Translation of the German original. The German original, which you can open as a PDF above, is the authoritative version.